What is temper Bead Welding (TBW) or Controlled Weld Deposition (CWD)
Performing welding repair on materials that are exposed to high temperatures is a challenging job. Most of the materials (Low alloy steel e.g. Cr-Mo types, Cr-Ni Alloys e.g. SS347, Incoloy 800, etc.), when exposed to high temperature during service, will result in aging and brittle microstructure due to various metallurgical changes.
Example applications of these materials are in power plants, refineries, and other related areas.
As we know Material properties get degraded when they are exposed to elevated temperature services e.g. in petrochemical, power plants & steel plants static equipment & piping. Due to the resultant inferior and degraded mechanical properties, performing welding of these materials is a very challenging task for the welding engineers because:
- Microstructure prone to change to martensite during welding repair.
- Controlling the weld & HAZ hardness.
- Minimizing the residual stresses.
- Controlling the grain refinement.
- Microstructure detrimental to toughness properties.
The best option to regain the mechanical properties such as strength, ductility, and toughness calls for the post-weld heat treatment (PWHT). But full PWHT is not possible due to in-service equipment operation, due to the size of equipment (Large size parts), the extent of the repair and material properties, etc.
So, it is always not an on-hand offer to make the heat treatment to bring back the material to its normal microstructure or stress conditions.
Definition of temper bead welding:
The definition of Temper Bead Welding is clearly stated in BPVC ASME Section IX Code. ASME Section IX, QG 109-Definitions, stated the Temper bead Welding as:
”a weld bead placed at a specific location in or at the surface of a weld for the purpose of affecting the metallurgical properties of the heat‐affected zone or previously deposited weld metal.’‘
Reference: ASME Section IX, QG 109 2019 Edition.
In simple words, this welding method is used, for many materials such as CS material, Cr-Mo alloys, and alloy steel when a PWHT is impractical due to service conditions or other limitations.
TBW helps to achieve various objectives by a pre-planned approach by:
- Placing weld beads at pre-determined locations.
- Tempering the base metal, preceding weld beads/ weld passes.
- Relieving the residual stresses.
- Controlling the weld cooling rates to eliminate hard microstructures.
Watch our YouTube video for interactive animation learning on Temper Bead Welding
Objectives of Temper Bead Welding
Temper Bead Welding’s main objective is to eliminate the need for post-weld heat treatment (PWHT) after weld completion where is mandatory to perform the PWHT due to material type, code requirement, or client specification.
In general, Temper bead welding serves to achieve the following objectives:
- Help to reduce as-welded HAZ hardness.
- Beneficial for repair welding for large structures for which it is difficult to perform the specified post-weld heat treatment.
- To refine the coarse-grained HAZ in the parent metal.
- Help to reduce residual stresses.
- Provide localize PWHT of previous weld beads.
What is a Temper Bead Welding?
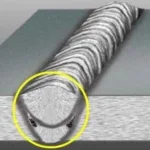
In temper bead welding, the heat input of successive layers temper previous beads, resulting in a fine grain structure and low hardness in the heat affected zone (HAZ).
This process is often used for welds that need to avoid post-weld heat treatment (PWHT). It can because of impractical PWHT situations such as welding repair in a in-service plant. Temper bead welding can produce welds with good mechanical properties and a small HAZ.
Temper Bead Techniques
There are a variety of temper bead techniques that can be used to achieve different results. Here are five of the most popular:
a) Half Bead Technique
b) Consistent Layer Technique
c) Alternate Temper Bead Technique
d) Controlled Deposition Technique
e) Weld Toe Tempering Technique
Qualification of Temper Bead Welding Procedures
Welding Procedure Specifications (WPS) and Procedure Qualification Records (PQR) are the foundation of a sound welding quality program.
In order to ensure that all qualified WPS results in required weldment properties, it is necessary to follow the requirements set forth in ASME Section IX. This section covers all details for WPS-PQR, including welder qualification, welding operator qualification, and production welding for Temper Bead welding qualification.
The first step in qualifying a temper bead welding procedure is to establish the base metal specifications. The base metal thickness, grade, and heat treatment must all be taken into account when determining the appropriate filler metal and weld parameters.
Once the base metal specifications have been established, the next step is to qualify the welder. The welder must be qualified in accordance with ASME Section IX before they can begin welding on production parts to carry out the temper bead welding.
Test Required for Temper Bead Procedure Qualification
A test is required for temper bead procedure qualification in order to assess the microstructure of the weld and heat-affected zone (HAZ). The hardness and CVN values are also important factors in determining the success of the temper bead procedure. The test results will help determine if the weld and HAZ can meet the required strength and toughness properties.
The bend test is used to determine the ductility of the weld metal. The Charpy V-Notch is used to determine the toughness of the weld metal.
A Summary of test generally required for Temper Bead Procedure Qualification are mainly as discussed above:
- Microstructural Test: For weld metal, HAZ and adjacent base metal
- Hardness Test: For weld metal, HAZ and adjacent base metal
- Charpy V-Notch Test
- Bend Test


Temper bead welding is a repair technique. Excellent explanation in this post to clear my doubts.
Which code covers temper bead welding applications in Oil & gas field?
Refer to API 510 clause 8.1.7.4.3 Preheat or Controlled-deposition Welding (CDW) Methods as Alternatives to PWHT.